×
Raised Hopper Direct Discharge Vibrating Sieve High‑Inlet Flow‑Thru Vibrating Screen for Powder Impurity Removal
In modern automatic powder processing workshops, the matching height between screening equipment and the upstream feeding pipeline has always been a key factor restricting production continuity. Many standard direct‑discharge vibrating sieves cannot adapt to high‑level feeding systems, requiring extra hoppers, conveyors and transition pipes, which increases investment cost and causes material residue and blockage during transfer.
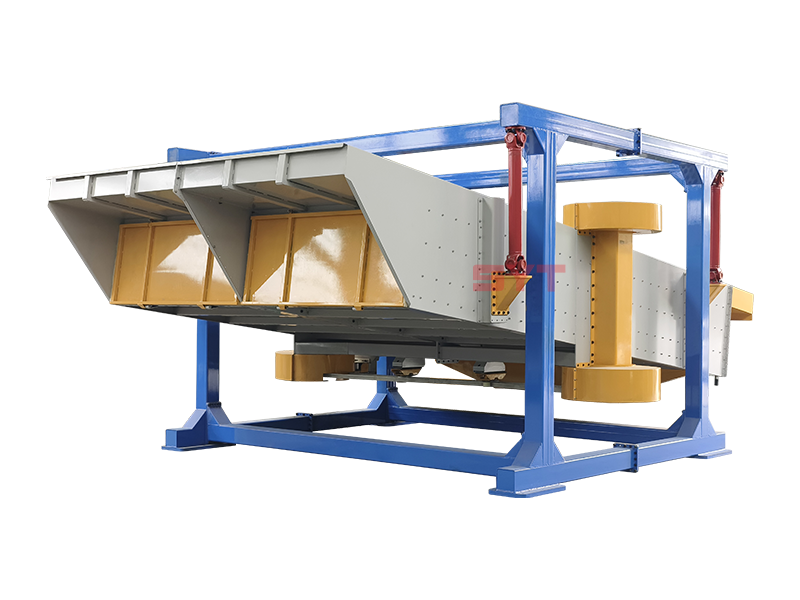
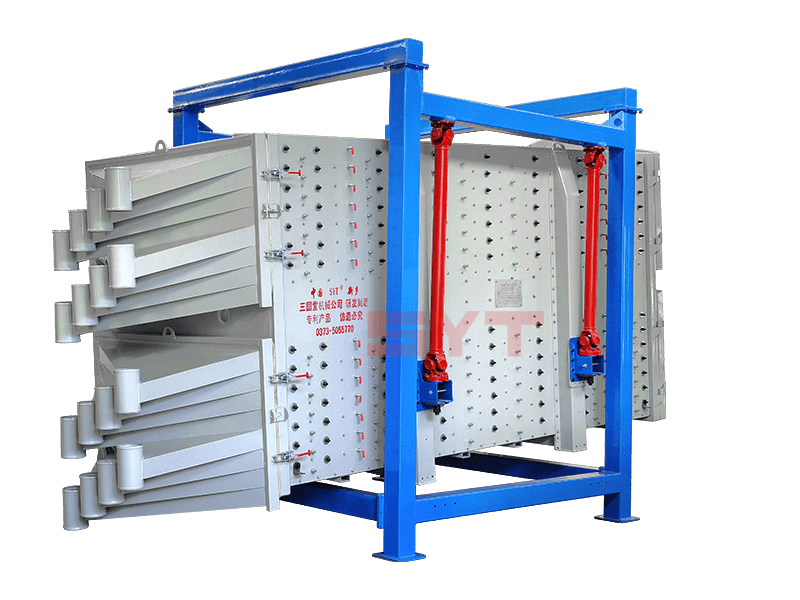
To solve this on‑site problem for our client, we developed this non‑standard heightened direct discharge vibrating sieve. Different from the conventional straight‑flow screen, this machine adopts an extended heightened body and raised feeding inlet. The overall height is fully customized to perfectly dock with the customer’s existing blanking pipeline. Raw materials can fall directly into the screening chamber by gravity without secondary conveying equipment.
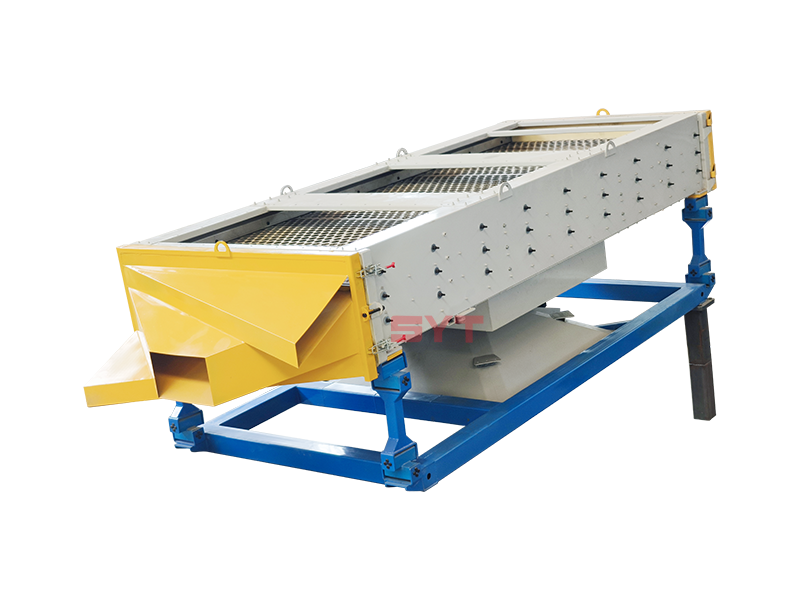
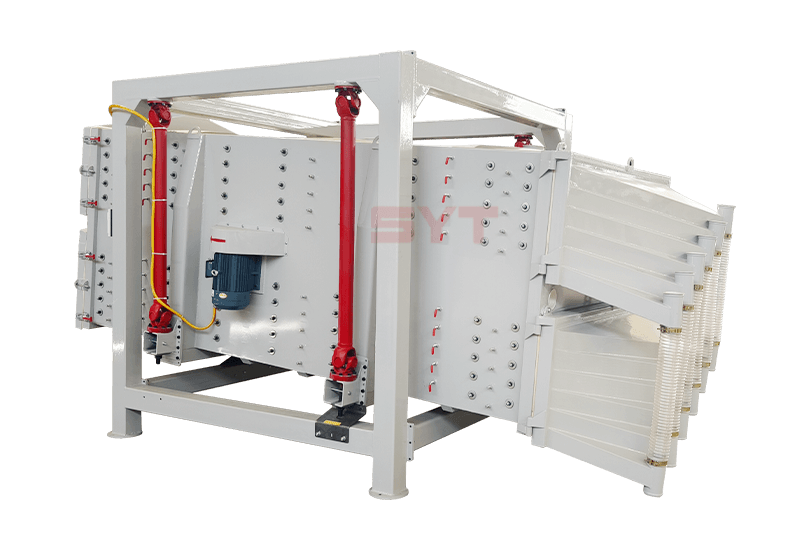
Equipped with double vertical vibration motors, the machine generates stable and powerful vibration force. After entering the sieve, powder materials are quickly dispersed on the screen surface for impurity removal and fine screening. Qualified fine materials flow vertically downwards and discharge directly from the bottom outlet to the next‑procedure packaging equipment. Coarse impurities and oversized particles are continuously pushed outward and discharged from the side slag outlet to realize uninterrupted continuous production.
This customized heightened direct‑discharge vibro sieve retains all advantages of the classic straight‑flow model: large throughput, compact structure, low noise and easy disassembly for screen replacement and internal cleaning. The quick‑clamp design ensures no dead corners inside the machine, which meets the hygiene requirements of food, starch, food additives and pharmaceutical‑grade powder production.
Our technical team provides one‑stop non‑custom services, including customized body height, feeding caliber, outlet direction, screen mesh number, explosion‑proof motors and stainless‑steel contact parts. We keep optimizing screening solutions according to different production capacity demands and workshop layout conditions.
After installation and commissioning on site, the equipment runs stably for a long time. It effectively improves the overall automation of the production line, reduces manual operation and material waste, and greatly raises the enterprise’s processing efficiency.
We keep offering professional vibrating screening equipment and tailor‑made separation solutions
for global customers in food, chemical, pharmaceutical, metallurgy and new‑energy industries.