×
Dust-Free Pneumatic Vacuum Feeder Project for Gyratory Sifter Supporting Line
Project Background
This overseas customer is a powder processing manufacturer from Southeast Asia, mainly engaged in the production of spice powder and food additives.
Before cooperation, the factory
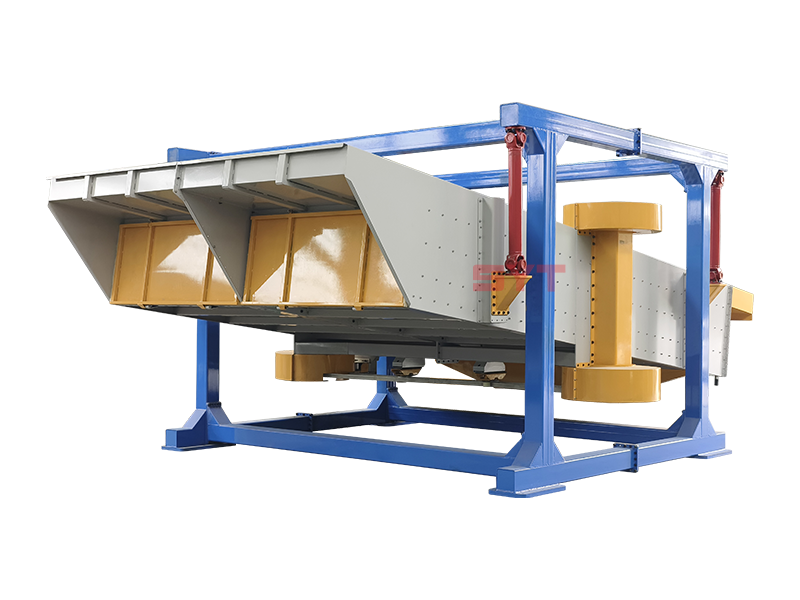
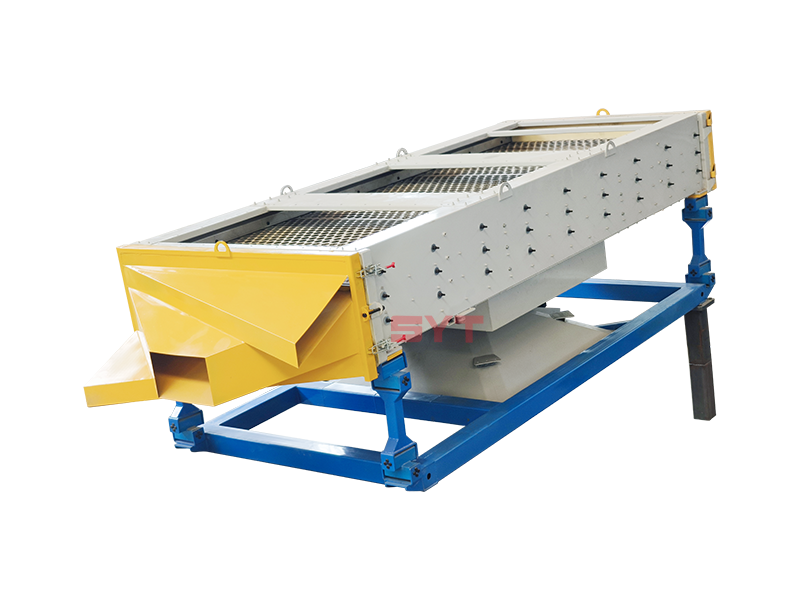
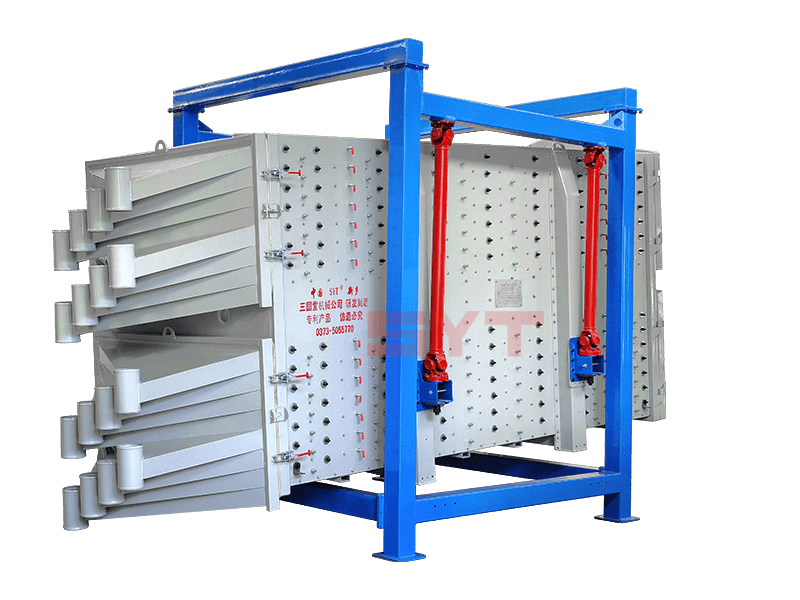
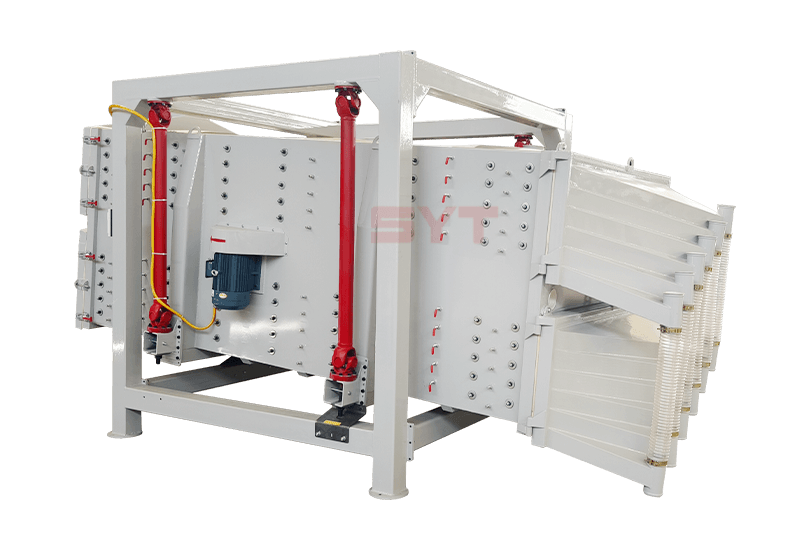
adopted manual bag dumping and feeding mode to transfer fine powder into the downstream horizontal airflow sieve and square gyratory sifter.
This traditional feeding method brought many long-standing troubles.
Workers needed to lift 25kg material bags repeatedly and pour powder into the sieve hopper manually. A large amount of fine dust floated
in the workshop during feeding, causing serious material loss. The dusty environment not only failed to meet local food hygiene standards,
but also brought occupational health risks to operators. Besides, manual feeding was unstable. The feeding speed fluctuated greatly, which affected
the screening precision and final yield of the airflow sieve. The customer tried several local suppliers, but the equipment could not adapt to slightly
sticky fine powder, and the filter was easy to block, with high maintenance frequency.
After comparing multiple Chinese manufacturers, the customer contacted us on Made-in-China. They needed a fully enclosed automatic vacuum
feeder to match their existing screening line, to realize continuous feeding for the horizontal airflow sieve and square swing sieve. Their core
requirements: dust-free closed conveying, easy disassembly and cleaning for food grade, stable feeding rate, compatible with multiple
powder materials, and simple operation for local workers.
Customized Solution
Combined with the customer’s material characteristics, production layout and matching screening equipment, our technical team
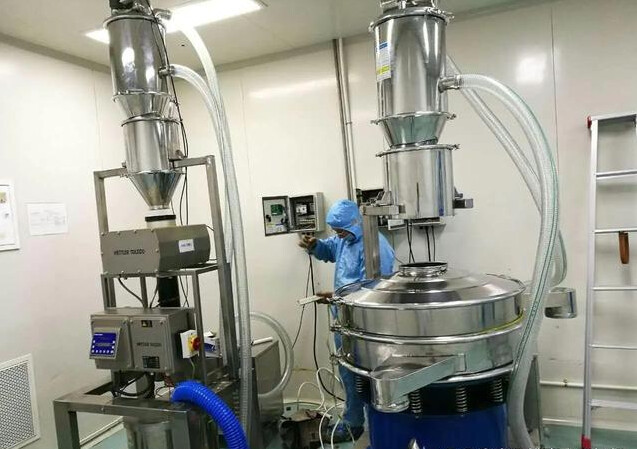
designed a set of vacuum feeding system. The contact parts of the machine adopt SUS304 food-grade stainless steel, which meets
food contact requirements. The vacuum feeder is connected by quick-clamp structure, convenient for full disassembly, washing
and material changeover, avoiding cross-contamination between different spice formulas.
We equipped the machine with pulse automatic back-blowing filter system. It can clean the filter cartridge regularly during continuous
operation, effectively solving the blockage problem of fine and slightly sticky powder. The PLC control panel supports adjustable feeding
speed and automatic material level detection. When the hopper of the downstream sieve reaches the set material level, the vacuum
feeder will pause feeding automatically; when the material is low, it will restart suction. It realizes interlocking and synchronous operation
with the airflow sieve and gyratory sifter, no need for special worker to watch the feeding station.
According to the customer’s site layout, we customized the conveying pipeline length and vertical lifting height. The whole pipeline is
fully sealed, no dust leakage. The supporting vacuum pump is equipped with silent treatment, which will not bring excessive noise to
the production workshop. We also reserved standard interfaces, so the customer can expand the feeding points and connect with
other mixers and screening machines later.
On-site Installation & Commissioning
After production and factory testing, the vacuum feeder was packed in export fumigation-free plywood case and shipped to the customer’s
factory. Our engineers provided remote video guidance for installation, wiring and commissioning. We sent detailed operation manuals,
maintenance videos and spare parts list in English.
During on-site test run, the customer put spice powder and additive powder into the feeding station. The vacuum feeder sucked powder
through negative pressure and stably delivered the material into the inlet of the horizontal airflow sieve. The whole feeding process
was clean, no dust overflow. The actual conveying capacity reached 300–800 kg/h, which fully met the customer’s production demand.
Local workers quickly mastered the operation, cleaning and daily maintenance steps under our online training.
Project Benefits & Customer Feedback
After one month of stable operation, the customer gave positive feedback.
First, the fully enclosed vacuum feeding eliminated dust pollution fundamentally. The material loss rate dropped sharply,
and raw material waste was greatly reduced. The workshop passed the local food hygiene inspection smoothly.
Second, labor cost was cut down. The original feeding station required two workers to work in shifts, now only one worker
is responsible for bag replacement, and the labor intensity is greatly reduced.
Third, the feeding speed is uniform and stable. Cooperated with our airflow sieve and square gyratory sifter, the screening
efficiency and grading accuracy are improved, and the product rejection rate is reduced.
Fourth, quick-release structure brings great convenience. When switching different powder formulas, disassembly and
cleaning can be finished quickly, which saves a lot of downtime.
The customer highly recognized our equipment quality